Short answer: KeystoneMold LLC, a Wyoming USA company run by a Taiwanese team, supplies ejector sleeves to ISO 8405 / DIN 16756, JIS or your drawing. Sleeves are machined at our Dongguan factory (DongGuan CT Mould): bore and outside diameter are both ground, the bore is matched to your core pin, and bore-to-OD concentricity is measured on a Hexagon CMM. Inspection report requirements are confirmed per order. One piece is fine for standard sizes.
Reviewed by Leon Wang, CEO & Technical Director, KeystoneMold LLC.
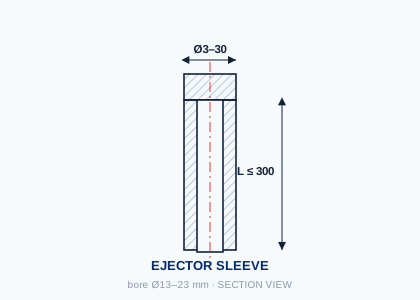
An ejector sleeve is a hollow pin that slides over a fixed core pin and pushes a round boss, tube or screw post off the core. Because it runs on two surfaces at once — the core pin inside and the ejector bore outside — it is less forgiving than a plain pin. Most sleeve problems come from bore clearance that is too tight or too loose, poor concentricity between bore and OD, thin walls on small sleeves, or a soft working surface on high-cycle or glass-filled jobs. That is why we quote a sleeve against the core pin it runs on, not as a standalone tube.
| Item | Typical range |
|---|---|
| Standards | ISO 8405 / DIN 16756 sizing; JIS-style; to drawing |
| Outside diameter (OD) | 3 – 30 mm typical |
| Inside diameter (bore) | 1.5 – 25 mm typical |
| Length | Up to 300 mm typical |
| Bore | Ground to match your core pin; H7-type fit or clearance as specified |
| Grinding | Confirmed per drawing / per order on critical diameters |
| Bore-to-OD concentricity | 0.005 mm target, measured on CMM; confirmed per drawing |
| Materials | SKD61 (≈H13 / 1.2344), SUJ2 (≈52100); others on request |
| Hardness (typical) | SKD61 through-hardened ≈HRC 50–55; SKD61 nitrided surface ≈900+ HV; SUJ2 ≈HRC 58–62 |
| Nitriding | Optional; case depth about 0.05–0.1 mm on request |
| Matching core pin | Can be supplied as a set with the sleeve |
| Inspection | Hexagon CMM + TESA optical available; inspection report requirements confirmed per order |
Values are typical. Send your drawing and we confirm against the actual requirement.
Inspection report requirements are confirmed per order. When a measured report is provided, it covers: bore diameter, outside diameter, bore-to-OD concentricity, head diameter and thickness, overall length and any step length — nominal, tolerance and measured value for each. See the format: sample inspection report.
| Order type | Typical range | What drives it |
|---|---|---|
| Standard sizes | ~7–15 working days ex-factory | Quantity, nitriding queue |
| Custom sleeves to drawing | ~10–20 working days ex-factory (typical) | Bore size, heat treatment, nitriding |
| Rush / repair replacement | Often a few working days for simple sleeves in small quantities | Steel on hand, nitriding yes/no |
| Express shipping to the US | Typically ~3–7 days after dispatch | Carrier, customs clearance |
We confirm the ship date with the quotation. If a rush date can't be met, we say so before you order.
Full guide: What to include in a mold component RFQ.
Our target is 0.005 mm between bore and outside diameter, measured on the Hexagon CMM; the achievable value depends on bore size and length, and we confirm it per drawing.
Yes. Send the core pin diameter with its tolerance (or the drawing) and the clearance you want; we grind the bore to match. If the core pin is worn, we can quote a new matched pin and sleeve set.
No — the standard sleeve is through-hardened. Nitriding is quoted as an option; we recommend it for glass-filled resins and high-cycle tools.
Our typical range starts at about 1.5 mm. Very small bores on long sleeves are limited by internal grinding; send the drawing and we will confirm.
Yes, to their published dimensions and materials, as equivalents — not branded parts. Send the part number and we confirm the details before quoting.
One piece for standard sizes; custom sleeves are quoted per drawing.
For a new customer we can make one free sample when appropriate, so you can check fit on your core pin before a larger order.
STEP / IGES / DWG / PDF accepted.
Request a Quote LinkedIn — Jaco DengBuying pins, sleeves and core pins for the same mold? Send one drawing pack — we quote and ship them together.